High-Turnover Isuzu Transmission & Engine Assembly Components
Each OEM-coded drivetrain component undergoes precision dynamic balance testing and ultrasonic metallurgical evaluation for uncompromising longevity.
The Global Commercial & Off-Highway Powertrain Environment
An authoritative analysis of Isuzu manual, automated manual (AMT), and heavy industrial transmissions across municipal logistics, mining platforms, and hydraulic earthmoving machines.
In modern industrial logistics and civil earthmoving, few mechanical assemblies operate under greater mechanical tortional stress than the internal combustion drivetrain. Isuzu Motors has dominated the medium-duty and light-commercial vehicle landscape through iconic manual platforms like the MYY-5T, MYY-6S, and MLD-6Q, alongside heavy-duty configurations such as the MEB-9 and MAL-6P. Simultaneously, the profound engineering alignment between Isuzu diesel engines (including the 4HK1, 6HK1, and 6WG1) and heavy earthmoving manufacturers like Hitachi (ZX series) necessitates synchronized transmission interfaces, pump drive gearboxes, and power take-off (PTO) mechanisms that endure thousands of continuous load-hours under high ambient temperatures and dusty conditions.
Global procurement teams currently face severe supply-chain bifurcation: escalating costs of direct dealership replacements coupled with long lead times, against the dangerous influx of sub-standard gray-market cast components that fail prematurely under torque shocks. A high-tier Isuzu transmission rebuild requires precision tolerance integration across the input shaft, countershaft cluster gears, main shaft, synchronizer sleeves, bronze blocker rings, and needle roller bearings. Operating without strict dimensional inspection can lead to premature helical gear pitting, synchro cone slippage, or catastrophic casing rupture.
Metallurgical Integrity
Fabricated from forged alloy steels such as 20CrMnTi and SNCM420, deep-carburized to 58-62 HRC. This guarantees micro-structural tooth toughness capable of handling torsional peak shock loads exceeding 1,450 N•m.
Micron-Grade Tolerances
Finished on CNC gear-grinding machinery conforming to DIN Class 6 / AGMA Class 11 specifications. Tooth profile crowning eliminates stress concentrations and drastically reduces transmission whining.
Rapid OEM Interchange
Cross-referenced against genuine Isuzu EPC catalogs and casting marks. Parts directly match OEM assemblies across N-Series (ELF), F-Series (Forward), and Giga heavy fleets, preventing costly return cycles.
Isuzu Transmission Spare Parts Quotation & Technical Matrix
Comprehensive overview of primary transmission sub-assemblies, OEM part numbers, core dimensional attributes, and wholesale benchmark quotations for international fleet purchasing.
| OEM Reference | Component Description | Target Transmission | Engine / Machine Pairing | Material / Spec | Status / MOQ |
|---|---|---|---|---|---|
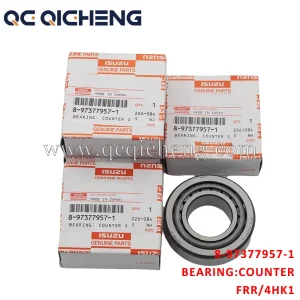
| 8-97377957-1 | Bearing, Counter Shaft Front | MLD-6Q / MYY-5T | 4HK1 / FRR, NQR Series | High-Carbon Chrome Steel (SUJ2) | In Stock (MOQ: 2) |
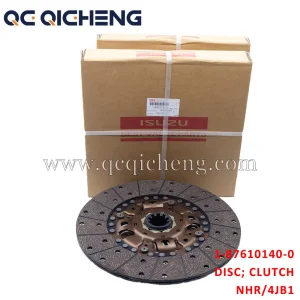
| 1-87610140-0 | Disc Assembly, Heavy Clutch | MYY-5S / MZZ-6 | 4JB1 / NHR, NKR Platforms | Cerametallic Multi-Friction Organic | In Stock (MOQ: 1) |
| 8-97252924-0 | Synchronizer Ring (2nd & 3rd) | MYY-6S / MYY-5T | 4JJ1 / N-Series Forward | Molybdenum Coated Dual-Brass | In Stock (MOQ: 5) |
| 8-98042456-1 | Input Shaft Sub-Assembly | MEB-9 / MAL-6P | 6HK1 / FTR, FVR Mining Haul | Forged 20CrMnTi, Case Hardened | In Stock (MOQ: 1) |
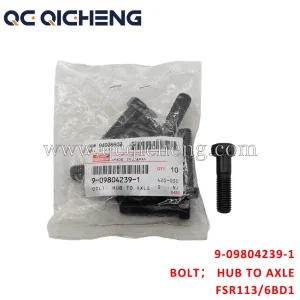
| 9-09804239-1 | Bolt, Hub to Axle Shaft | Axle & Transmission Output | 6BD1 / FSR113 Commercial | Grade 10.9 Tensile Steel, Zinc Chromate | In Stock (MOQ: 20) |
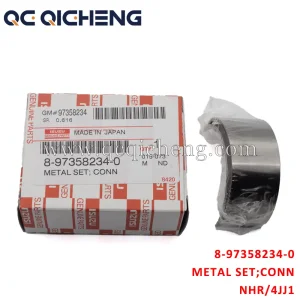
| 8-97358234-0 | Connecting Rod Metal Bearing Set | Crank-to-Drivetrain Transfer | 4JJ1 / NHR Commercial Fleet | Tri-Metal Sintered Copper-Lead/Al-Sn | In Stock (MOQ: 1 Set) |
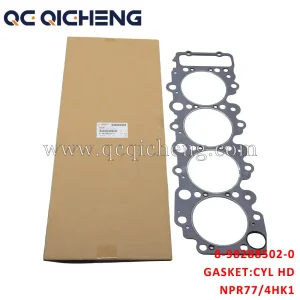
| 8-98288502-0 | Multi-Layer Steel Cylinder Head Gasket | Compression Seal Interface | 4HK1 / NPR77 Transport Units | Multi-Layer Spring Steel with Viton Coating | In Stock (MOQ: 2) |
Technical Metallurgy & Wear Resistance Engineering
In heavy-duty applications, transmission components must resist pitting, gear tooth bending, and spalling. Case-carburization treatment for our Isuzu-compatible gears yields an outer hardened case depth of 0.8 mm to 1.2 mm with a core hardness of HRC 32–40. This distinct duality provides a wear-resistant diamond-hard contact flank, while the ductile core readily absorbs torsional shock waves caused by sudden deceleration or erratic payload shifts.
Synchronizer rings feature double-cone and triple-cone configurations lined with sintered carbon friction material or molybdenum sprays. This design enhances synchronization friction coefficients up to μ = 0.12, dissipating kinetic slip energy quickly and minimizing transmission shift lever throw during fast, uphill shifts.
Localized Applications & Field Failure Prevention
Specific environmental conditions require adapted transmission rebuild strategies. Here is how our components perform in demanding global territories.
Tropical & High-Humidity Logistics
Region: Southeast Asia, Equatorial Africa, Central America.
Stress Point: Extreme ambient humidity leads to moisture condensation inside transmission vent breathers, causing oil emulsification.
Solution: Viton® fluoroelastomer oil seals with double-lip dust ejectors, paired with phosphate-coated gear journals that prevent micro-corrosion during high-idle operations.
Arid, High-Dust Mining & Quarrying
Region: Middle East, Western Australia, Atacama Desert.
Stress Point: Fine silica particles penetrate standard bell-housing seals, causing severe abrasive wear on clutch release bearings and scoring countershafts.
Solution: Induction-hardened countershaft journals with labyrinth seals and heavy-duty throw-out bearings loaded with high-temperature synthetic polyurea grease.
Sub-Zero Regional Distribution
Region: Nordic Europe, Northern Canada, Central Asia.
Stress Point: Cold start-ups create high oil shear resistance, causing synchronizer ring lockup and initial gear engagement failure.
Solution: Carbon-fiber-lined synchronizer friction rings that engage reliably across extreme temperature ranges (-40°C to +130°C) without material delamination.
Enterprise Drivetrain Procurement: Mitigating Fleet Downtime
A systematic framework for fleet managers, municipal transit authorities, and heavy excavation contractors to eliminate unexpected mechanical failures.
For operations running fleets of 20 to 500 Isuzu-powered vehicles, transmission failures are rarely limited to the component purchase price alone. An unplanned transmission seizure on a commercial delivery route or remote mining site triggers significant indirect costs: emergency towing, operator overtime, missed logistics penalties, and secondary driveline damage to propshafts and differential ring gears.
To reduce Total Cost of Ownership (TCO), leading logistics fleets use a Structured Rebuild Lifecycle Program. Instead of replacing single worn gears reactively, maintenance technicians install synchronized overhaul kits during scheduled 300,000 km overhauls. A standard overhaul kit includes: input shaft bearing, countershaft front/rear bearings, main shaft pilot bearings, complete synchronizer blocker ring sets, dynamic oil seals, and genuine gasket rings.
Part Number Cross-Verification
Every quote request is cross-checked against Isuzu Global EPC data using vehicle VINs, chassis numbers, and transmission casting codes, preventing mismatched parts and costly customs returns.
100% Quality Assurance
All rotating parts undergo Coordinate Measuring Machine (CMM) dimensional validation, profile roughness tests, and ultrasonic crack detection to verify microstructural integrity prior to export packaging.
Consolidated Global Logistics
We provide unified packing across multi-SKU orders (combining transmission shafts, synchros, engine sensors, and water pumps) with compliant customs paperwork for rapid export clearance to 120+ countries.
Isuzu Heavy Commercial & Excavator Powertrain Components
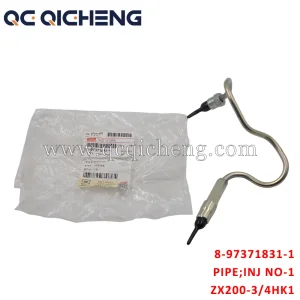
Complete your fleet drivetrain order with precision-matched valvetrain assemblies, fuel delivery lines, structural brackets, and heavy clutch discs.
Frequently Asked Questions: Isuzu Transmission Rebuilds & Procurement
Comprehensive engineering guidance on part identification, lubrication, gear backlash settings, and global ordering processes.